
How Coolant Chemistry Has Evolved in Heavy-Duty Equipment
A heavy-duty engine built several decades ago and a modern diesel engine may perform similar jobs, but their cooling system requirements aren’t necessarily the same.
Engine designs have changed. Manufacturers have introduced different materials, tighter engineering tolerances, and new operating requirements. Equipment also spends long hours working under heavy loads, often in environments where heat, dust, and demanding service conditions are part of everyday operation.
Coolant technology has had to keep pace.
Coolant technology has evolved from basic freeze protection into a range of formulations with different corrosion inhibitor systems, service requirements, and application specifications.
Understanding coolant chemistry helps explain why modern maintenance teams pay closer attention to the type of fluid going into an engine. The right heavy-duty coolant isn’t simply about keeping temperatures under control. It’s also about protecting internal surfaces and maintaining the condition of the entire cooling system over time.
Overview
- Heavy-duty coolant has evolved as engine designs and cooling system requirements have become more demanding.
- Traditional formulations relied on different corrosion inhibitor packages, while newer technologies introduced alternative approaches to long-term protection.
- OAT and other modern coolant technologies offer different maintenance requirements and protection characteristics.
- Choosing coolant based on engine specifications and compatibility remains essential for reliable cooling systems.
Early Coolants Focused on Basic Temperature Protection
Early antifreeze formulations were primarily concerned with protecting engines against freezing and helping prevent overheating. Ethylene glycol became a widely used base fluid because of its ability to lower the freezing point and raise the boiling point of a coolant mixture.
However, glycol alone doesn’t provide all the protection an engine cooling system needs.
Coolant circulates through passages containing different metals and comes into contact with surfaces that can be vulnerable to corrosion. Without suitable inhibitors, the fluid can contribute to deterioration rather than simply protecting the engine.
As heavy-duty diesel engines became more widely used, additional concerns emerged. Cooling systems needed protection against corrosion, deposits, and cylinder liner pitting, particularly in engines operating under demanding loads.
This led to the development of coolant formulations containing more carefully selected additive packages.
The focus gradually expanded beyond basic temperature control to include:
- Corrosion protection for metal surfaces.
- Control of scale and deposits.
- Freeze and boiling-point protection.
- Support for heat transfer.
- Protection against diesel engine liner pitting where required.
The chemistry became more specialized because the equipment itself demanded more from its cooling system.

Conventional Coolants Introduced More Advanced Inhibitor Packages
Conventional heavy-duty coolants improved on basic antifreeze by incorporating corrosion inhibitors designed to protect cooling system components.
Depending on the formulation, these packages may include silicates, phosphates, nitrites, and other additives. Each has a particular role in protecting the surfaces and materials found inside an engine’s cooling system.
Nitrite, for example, has traditionally been important in many heavy-duty diesel applications because it helps protect cylinder liners against cavitation-related pitting. Silicates can provide corrosion protection, particularly for certain metal surfaces.
These formulations offered practical protection, but their additive chemistry required attention during service.
As inhibitors were consumed or depleted, coolant condition could change. Some conventional heavy-duty coolant programs require periodic testing and, when needed, supplemental coolant additives (SCAs) to maintain the required protection.
For maintenance teams, that meant keeping track of more than just coolant levels.
A typical conventional coolant maintenance routine could involve:
- Checking coolant concentration.
- Monitoring inhibitor levels.
- Testing nitrite protection where applicable.
- Adding approved SCAs when required.
- Following the specified coolant replacement schedule.
These practices remain relevant for equipment using conventional coolant technology. The important point is that different formulations require different maintenance approaches.
Organic Acid Technology Changed the Approach to Corrosion Protection
One of the significant developments in coolant chemistry was the wider adoption of Organic Acid Technology, commonly known as OAT.
OAT formulations use organic acid corrosion inhibitors to protect cooling system surfaces, while conventional and hybrid formulations may use different combinations of inorganic and organic inhibitors.
This approach changed how manufacturers designed certain extended-life coolants.
Rather than relying on the same combination of traditional additives, OAT formulations use a different inhibitor strategy intended to provide longer-lasting corrosion protection under approved operating conditions.
Some of the characteristics associated with OAT technology include:
- Extended coolant service potential.
- Corrosion protection for wetted cooling system surfaces.
- Reduced reliance on traditional inhibitor packages.
- Different testing and maintenance requirements.
- Formulations designed for particular engine specifications.
It’s important to understand that OAT is not a single universal formula. Different products can use different inhibitor combinations. Some heavy-duty OAT coolants include supplemental nitrite for diesel liner protection, while others are formulated without nitrite.
That distinction matters when selecting coolant for a particular engine.
Extended-Life Coolants Reduced Some Traditional Maintenance Demands
One of the reasons extended-life formulations gained attention was the opportunity to simplify certain aspects of coolant maintenance.
Traditional heavy-duty coolant programs could involve regular monitoring and replenishment of supplemental additives. Extended-life technologies introduced different inhibitor systems designed to maintain corrosion protection for longer service periods.
For equipment operators, this can make maintenance planning more straightforward.
Longer service intervals, where approved by the equipment manufacturer, may reduce the frequency of coolant replacement and some associated maintenance work. However, extended life doesn’t mean unlimited service life or the absence of inspections.
Maintenance teams still need to follow the manufacturer’s requirements and monitor coolant condition when recommended.
When working with extended-life formulations, they should consider:
- Whether the coolant meets the engine manufacturer’s specification.
- The approved service interval.
- Compatibility with the coolant already in the system.
- Whether supplemental additives are required.
- The appropriate testing procedure.
- Correct flushing and filling practices when changing technologies.
Mixing different coolant technologies without confirming compatibility can alter the intended inhibitor balance. A product’s extended-life designation should never be treated as permission to use it in every engine.
Modern Heavy-Duty Coolant Is Designed Around Specific Engine Requirements
Today’s heavy-duty equipment includes a wide range of engine designs and applications. Long-haul trucks, delivery vehicles, mining machines, agricultural equipment, and standby generators don’t all experience the same operating conditions.
Coolant formulations have evolved to address these different requirements.
Some products use conventional inhibitor technology, while others use OAT, hybrid, or other specialized approaches. Certain heavy-duty formulations combine organic acid inhibitors with nitrite to address diesel liner pitting, while nitrite-free OAT formulations use a different protection strategy.
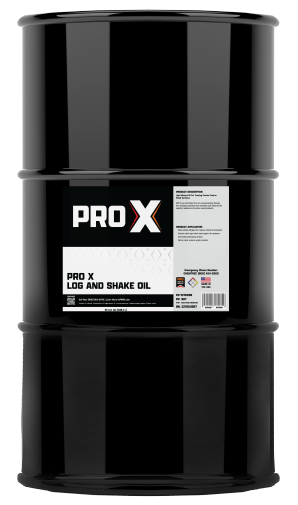
For example, PRO X HD ELC 50/50 A/F RED is a premixed heavy-duty extended-life coolant that combines organic acid technology with nitrite and silicate inhibitors. It is formulated to provide freeze, overheating, corrosion, and diesel engine liner-pitting protection. Its ready-to-use 50/50 mixture eliminates the need to prepare a coolant mixture during routine filling.
The selection process should always begin with the equipment requirements.
A maintenance team should check:
- Required coolant specification.
- Engine manufacturer approval or recommendation.
- Coolant technology and inhibitor package.
- Compatibility with the existing fluid.
- Required concentration.
- Service and testing intervals.
The objective isn’t to choose the newest chemistry available. It’s to choose the formulation designed for the engine being maintained.
Why Coolant Compatibility and Maintenance Still Matter
The evolution of coolant chemistry has given equipment operators more choices, but it has also made product selection more important.
Two coolants can have similar colors and still use different inhibitor technologies. Adding one formulation to another without checking compatibility can affect the intended protection.
This is particularly important when equipment has a long service history and previous maintenance records are incomplete.
Before changing coolant technology, maintenance teams should establish what’s currently in the system and whether the new formulation is approved for that application.
Good maintenance practices include:
- Identifying the existing coolant before topping off.
- Avoiding color-based product selection.
- Following manufacturer-approved flushing procedures when necessary.
- Using the correct coolant concentration.
- Testing coolant with a method suitable for its technology.
- Recording product changes and replacement dates.
Coolant condition also needs to be considered alongside the mechanical condition of the cooling system. A damaged radiator, restricted airflow, failing pump, or leaking hose can still create problems regardless of how advanced the coolant formulation may be.
Modern chemistry improves the options available to equipment operators, but proper maintenance remains essential.
Coolant Chemistry Continues to Evolve
Coolant technology has come a long way from its early focus on basic freeze and boilover protection. Modern formulations are designed with corrosion control, liner pitting prevention, heat transfer, and service requirements in mind.
For heavy-duty equipment operators, this evolution has created more specialized choices and, in some applications, opportunities for simpler maintenance programs.
Still, no single formulation is right for every engine. The correct heavy-duty coolant must meet the manufacturer’s requirements and provide the protection expected from that particular cooling system.
Understanding coolant chemistry helps maintenance teams recognize why conventional, hybrid, and OAT formulations are not automatically interchangeable and why the correct service procedure matters.
Ultimately, reliable cooling systems depend on more than the fluid itself. Suitable coolant selection, regular inspections, proper handling, and consistent maintenance all work together to protect equipment that is expected to perform day after day.